Hey there, if you’ve ever stood next to a running radiator fin forming machine, you know it’s equal parts workhorse and precision nut—one tiny hiccup, and you’re looking at messed-up fins that can ruin an entire batch of radiators. As a supplier of these machines, I’ve spent years walking clients through the messiest, most critical part of the job: process monitoring for radiator fin forming. It’s not just staring at a screen (though that’s part of it) — it’s the difference between cranking out 10,000 perfect fins an hour and having a line go down for 3 hours over a weirdly shaped die. Let’s break this down like we’re talking over a coffee, no jargon dump promise. Radiator Fin Forming Machine

First, let’s get on the same page about what we’re even monitoring here. Radiator fins are those thin, wavy metal sheets (usually aluminum, sometimes copper) that sit between radiator tubes to maximize heat transfer. They’re cut, shaped, notched, and stacked at lightning speed—some machines run 600+ fins a minute. So when I’m talking about process monitoring for these machines, I’m not talking about checking if the motor’s on. I’m tracking every single step of forming, because even a 0.1mm deviation in fin height or notch angle means it won’t slot right into the radiator core, leading to leaks, overheating, or full-on part failure.
Let’s start with the basics that everyone overlooks: real-time dimensional checks. Old school? You’d stop the line every hour, pull a fin off, measure it with calipers, cross your fingers. Today? We use high-speed vision systems mounted right at the forming station—cameras that snap a pic of each fin as it comes off the die, analyze it in milliseconds, and flag if it’s too tall, too short, or has a wonky notch. A lot of our clients think “vision is overkill,” until they run a batch of 5,000 fins that all have 0.2mm misaligned notches because a die screw worked loose mid-shift. The vision system caught it at fin 12, not fin 5,000. We also work with clients who add laser micrometers to track fin thickness—aluminum is soft, so a tiny variation from the coil can make the forming rollers slip, and laser monitors that in real-time too. Here’s the thing: this isn’t just for quality control. It’s predictive maintenance too. If the vision system notices 10 fins in a row are just barely over height, that’s a warning the die needs a polish, not that you need to scrap a bunch of parts.
Next up, force and load monitoring, which is the unsung hero of this process. When a fin is being formed, the rollers and dies exert a specific amount of force to bend it into shape. Too little, and it’s flat or not wavy enough. Too much, and you stretch the metal so thin it cracks—especially with the thinner gauges (like 0.1mm aluminum) that everyone’s using now to cut costs and weight. We fit our machines with load cells at every critical forming roller and the cutting die—these are little sensors that measure force in real-time, and if it spikes or drops outside the preset range, the machine slows down or stops before it ruins the fin. Last month, a client of ours was running a batch of copper fins (tougher than aluminum, so they need more force) and a load cell caught a sudden 20% drop in force—turned out a bearing in the forming roller was seized, and the machine was about to grind itself to pieces. If they hadn’t been monitoring force, they would’ve kept running until the bearing exploded, which would’ve cost them a $10k repair and 2 days of downtime. That’s the stuff no one tells you about process monitoring—it’s not just about good parts, it’s about keeping the machine running.
Then there’s material and coil feed monitoring, which sounds boring but is huge. Radiator fins come on big coils of metal, right? If the feed mechanism that pulls the coil through the machine slips even a tiny bit, every fin after that is going to be off by the same amount. We use encoders to track how much material is being fed in—like, exact millimeter-by-millimeter counts—and if the feed is off by more than 0.05mm, the machine alerts you. We also add material thickness sensors that check the coil’s thickness as it’s being fed in, because a coil that’s the wrong gauge (like 0.12mm instead of the ordered 0.1mm) will mess up the forming force we talked about earlier. I once had a client get a bad batch of aluminum coil from their supplier—they caught it immediately because our machine’s thickness sensor flagged it, instead of running all the fins and realizing at the end they couldn’t be used. That saved them from a $2k scrap bill and a late delivery penalty.
Wait, let’s talk about common mistakes we see clients make with monitoring. A lot of people go for the cheapest sensors they can find, and that’s a trap. Those cheap vision systems can’t handle the high speed of modern forming machines—they lag, so they miss defects. Or they set the tolerances way too tight, so the machine stops every two minutes over a tiny variation that doesn’t affect performance, leading to more downtime than it’s worth. We work with clients to set tolerance bands that are specific to their application, not a one-size-fits-all. For example, a client making fins for a small car radiator can have a 0.1mm height tolerance, but a client making heavy-duty truck radiator fins needs a 0.05mm tolerance because those trucks carry more weight, so the fins have to fit perfectly. We calibrate the sensors for their exact needs, not just our machine.
Also, data logging is a big part of monitoring that most people sleep on. Every time the machine detects a deviation, it logs what fin it was, what time, what the force was, what the material thickness was. That data is gold for troubleshooting. If a client starts getting a bunch of defective fins after a new shift starts, they can pull up the logs and see if the force was too high because that operator adjusted the rollers wrong, or if the feed was slipping because the coil wasn’t loaded right. We give our clients easy-to-use dashboards—no fancy IT degree needed—to pull this data, even on their phones. A client in Ohio told me last month he checks his machine’s monitor on his way to work, and if he sees a tiny spike in force, he can call his operator before he even gets to the plant to adjust it, instead of dealing with downtime.
Wait, let’s address the elephant in the room: why does this even matter? Radiator fins are a tiny part of a big system, but if they’re bad, the whole radiator is bad. I’ve seen radiator manufacturers get rejected by car makers because their fins were off—costing them millions in contracts. Process monitoring isn’t just a “nice to have” for a forming machine; it’s required if you want to make parts that work consistently, meet industry standards, and keep your production line running. As a supplier, we don’t just sell machines—we sell the monitoring setup that keeps our clients from losing sleep over bad parts or downtime.
Another thing: predictive vs. reactive monitoring. A lot of people think monitoring is just reacting to defects, but the best stuff is predicting problems before they happen. For example, if the load cells show that the forming force is increasing slowly over time, that means the die is getting worn out, so you can schedule a die change during a planned shutdown, not when the line is full of parts that need to get out. We use AI algorithms (nothing too fancy, just ones trained on our machines’ data) to spot these slow trends—like, if the force has increased 5% in 10,000 fins, that’s a warning sign. No more guessing when to change dies, which saves clients hours of downtime and extends the life of their dies, too.
Let’s throw in a real example from last quarter. We had a client in Texas running 800 fins a minute for commercial truck radiators. Their old machine didn’t have proper monitoring, and they were getting about 2% defect rate, which might not sound like much, but that’s 200 bad fins every 10,000, on a 100,000-fin order for a truck fleet. They switched to our machine with our monitoring setup, and within a week their defect rate dropped to 0.1%. That’s 10 bad fins per 100,000, saving them $15k in scrap and rework, plus they finished the order 2 days early. That’s the kind of difference good process monitoring makes.
Now, let’s talk about what’s not part of this—because people try to add stuff that’s useless. You don’t need to monitor the room temperature (unless you’re working in a warehouse that’s freezing, which can make aluminum brittle and affect forming, but that’s a side note). You don’t need to monitor every tiny motor vibration unless it’s causing a problem. The key is focusing on the variables that directly affect fin quality and machine health: dimensions, force, feed, material specs. That’s it—no overcomplicating it.
Wait, for anyone who’s new to radiator fin forming, let’s clarify one thing: the forming process itself is just a series of steps. First, the coil is fed into the machine, straightened, then cut to length. Then it goes through a series of roller dies that bend it into the wavy shape, followed by notching (for where the tubes will slot in), and then it’s stacked or collected. Each of these steps is where deviations can happen, so monitoring is placed at each of these stations. Our machines have dedicated monitoring zones: feed zone, straightening zone, forming zone, cutting zone. Each zone has its own sensors, so you can pinpoint exactly where a problem is, instead of guessing “the machine is broken.”
I’ll be honest, when I first started in this business, I thought process monitoring was just a marketing trick to sell more expensive machines. But after working with dozens of clients, I get it. For small shops, maybe they can get by with manual checks for a while, but once they start scaling, that’s when the problems hit. For large manufacturers, downtime costs tens of thousands of dollars an hour, so investing in good monitoring is non-negotiable. As a supplier, we tailor the monitoring setup to your needs: if you’re a small shop making 1,000 fins an hour, we can use simplified, cost-effective sensors. If you’re a big plant making 100,000 fins an hour, we can add high-speed vision, AI predictive tools, and full data integration with your plant’s system.
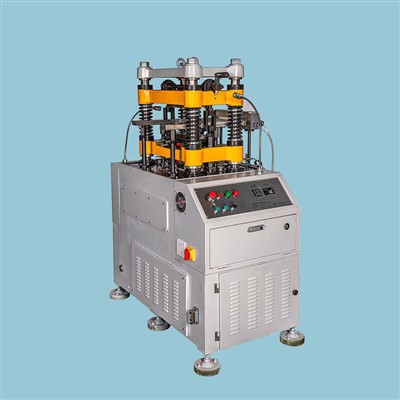
Let’s wrap this up. Process monitoring for radiator fin forming machines isn’t some black-box tech—it’s about seeing what’s happening at every step of forming, so you can make good parts, avoid downtime, and keep your production running smoothly. If you’re tired of scrapping batches of fins, dealing with unexpected line stops, or guessing when to replace parts, we can help you set up the right monitoring for your machine. Hit us up to talk through your setup, get a demo, or ask any questions—no sales pitch, just real talk about making your radiator fin operation work better.
Servo Cutting Machine REFERENCES
- Automotive Manufacturing Solutions. (2022). "Precision Forming of Heat Exchanger Fins: Key Variables and Monitoring Techniques."
- Metal Forming Magazine. (2023). "Real-Time Process Monitoring for Thin-Gauge Aluminum Forming."
- Society of Manufacturing Engineers (SME). (2021). "Quality Control in High-Speed Heat Exchanger Component Production."
Suichang Lvye Machinery Co., Ltd.
We are one of the most professional radiator fin forming machine manufacturers in China, also support customized service with low price. We warmly welcome you to buy discount radiator fin forming machine for sale here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No. 402, Mudanting East Road, Miaogao Street, Suichang County, Lishui City, Zhejiang Province
E-mail: L528753@outlook.com
WebSite: https://www.suichanglvye.com/
