Hey everyone, I’m Jake from Weigh Module Kits – and if you’re here, odds are you’re tired of dealing with wonky, disconnected weight data that throws your whole PLC process off. I’ve been on the supplier side of weigh modules for over 8 years, and let me tell you, integrating a weigh module kit with a PLC isn’t just hooking up wires and hoping it works. Skip the generic PLC tutorials; this is the stuff I’ve actually walked clients through, the mistakes we’ve fixed, and the quick wins that save you hours (or days) of downtime. Weigh Module Kits
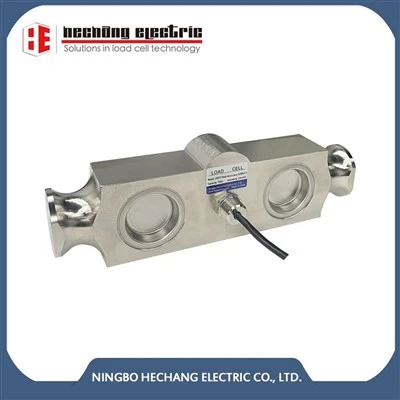
First, let’s ground this in what’s actually happening when you integrate these two. Weigh module kits are made of load cells, junction boxes, and maybe a signal conditioner – all that stuff takes the tiny, squishy millivolt signals from pressing on a load cell and turns it into a number a machine can read. A PLC (Programmable Logic Controller) is the brain of your whole operation – think bottling lines, conveyor systems, hopper batching for food or chemicals, even warehouse storage scales. The big, universal mistake new integrators make? Treating the load cell as just another I/O device, not a delicate sensor that needs to play nice with the PLC’s input specs.
Let’s start with the basics you actually need before lifting a screwdriver. No, this isn’t “read the manual” – it’s the pre-work that 90% of people skip. First, confirm your PLC’s input type. Do you have a Modbus RTU port? A 4-20mA analog input? A load cell-specific digital input? I’ve seen folks show up with a weigh kit that only outputs digital Modbus, and plug it into a basic analog PLC input, and wonder why the weight is all over the place. That’s a quick misstep that’s 100% avoidable. Second, check your power supply. Load cells are finicky – most need a regulated 5V DC, not the 24V DC that runs your PLC’s digital outputs. If you use the wrong power, you’ll get distorted signals, zero point drift, or even fried the load cell (yep, we’ve replaced half a dozen that happened from that exact mistake). Third, match the weight capacity of your module to your application. If you’re batching 500lb of flour, don’t buy a 10,000lb module – it’ll be less accurate, and the PLC will have to scale a tiny signal over a huge range, leading to noise. We usually tell clients: pick a module that’s 1.5x your max operating weight, that’s the sweet spot for accuracy without wasting budget.
Okay, pre-work done – now physical installation, the part where a lot of people cut corners. Let’s talk wiring first. Old school people use regular stranded wire; use shielded, twisted-pair wire for your load cells. Why? Because factories are full of electrical noise – VFDs, motors, conveyor drives – that will mess with your signal like a toddler with a radio. Twisted pair cancels out that noise, and the shield grounds it so it doesn’t bounce around. Another quick tip: keep the wiring runs for load cells separate from power wiring. If you have to run them in the same conduit, cross at 90 degrees only – never run parallel. Parallel runs let noise bleed into the signal line, and you’ll never figure out why your weight readings are flaky.
Now, mounting the weigh module. This is make-or-break. If it’s not mounted level, you’re getting uneven load on the cells, which means bad data. Use a bubble level, not a phone app (I’ve seen those app levels be off by 2 degrees – that’s enough to throw your accuracy off). Also, make sure you’re using the right mounting hardware – don’t just bolt it to whatever’s available. We supply mounting brackets specifically for our weigh kits, and I swear by them. They prevent side load (if something knocks into your conveyor, the bracket absorbs it instead of pushing the load sideways, which messes with the load cell’s calibration). If you skip that bracket, you’re setting yourself up for calibration headaches down the line. Oh, and one thing no one tells you: leave a tiny bit of slack in the load cell wiring, not tight. If the machine shifts during operation, tight wiring will pull on the cell and throw off zero.
Once the wires are run, signal conditioning. Most of our weigh module kits come with a built-in signal conditioner, but if you’re using a standalone load cell, you’ll need to add one. The conditioner’s job is to amplify the tiny millivolt signal from the load cell into something the PLC can read – 4-20mA, Modbus, or a digital signal. Here’s a trick: set the conditioner’s gain and offset first, before connecting to the PLC. Gain is how much you boost the signal; offset is the zero point. If you adjust these now, you don’t have to mess with the PLC later, which saves time. Pro tip from my team: use a precision digital multimeter to test the signal before hooking it to the PLC. If you’re getting a stable 4mA with no load and 20mA with a test weight, the signal’s good – if not, tweak the conditioner’s trim pots. No point hooking a bad signal to the brain first.
Now the PLC side, the actual software stuff. I’m not gonna get too deep into ladder logic, but here’s the stuff that matters. First, set up the PLC’s input module correctly. If it’s an analog input, set the range to match your module – 0-10V, 4-20mA, whatever your kit uses. If it’s Modbus, make sure the slave address matches the one set on your module’s DIP switches – I’ve seen half a day wasted because two modules had the same slave address, so the PLC was pulling data from the wrong one. Second, create a scaling block in the PLC. A lot of people just take the raw analog value (like 12000) and call it pounds, but that’s wrong. Let’s say your module’s max is 500lb, and the PLC’s analog input goes from 0 to 32767 for 4-20mA. You’d set the scaling to go from 4mA (raw 6553) = 0lb, 20mA (raw 32767) = 500lb. That takes two seconds, and makes your weight readings accurate. Third, add filtering. Factories have so much movement – conveyor vibration, product shifting – that the raw weight signal bounces. Most PLCs have a simple moving average filter, or you can add a threshold so it only updates the weight if it changes by, say, 0.5lb. Too little filtering, and your HMI screen looks like a stock chart; too much, and it takes 10 seconds to register a new batch. We usually test with the actual operating conditions first – run the conveyor for 5 minutes, see how much it bounces, then set the filter accordingly.
Calibration is the final step, and this is where a lot of integrators cut corners. I see people just taring the module and calling it good – no, you need a certified test weight. If you’re batching 100lb, use a 100lb test weight (or a stack of smaller ones that add up to exactly that) to calibrate. Here’s how we do it: first, make sure there’s no load on the module, hit the tare in the PLC (that sets zero). Then, set a test weight on the module, enter the exact weight in the PLC’s calibration menu, and it adjusts the scaling so the raw value matches the test weight. This is non-negotiable – if you skip this, your weight readings will be off by 5-10% minimum, and you’ll have to re-calibrate every week. Also, after calibration, do a quick check with a random test weight – if it’s 5lb off, you messed up the scaling, not the module.
Now, common issues we fix every week, so you don’t have to. First, zero drift. If your weight keeps creeping up or down, check for loose wiring, power fluctuations, or not enough filtering. 9 times out of 10, it’s a bad ground on the shield – use a multimeter to make sure the shield is only grounded at one end (not both, that creates a ground loop which causes noise). Second, inconsistent readings. If the PLC shows different weights when you set the same test weight, check for side load – is the module mounted level? Is there something rubbing against it? Third, Modbus communication errors. If the PLC isn’t pulling data from the module, check the baud rate, parity, and stop bits – they have to match on both the module and the PLC. Most people forget to set parity, which kills half their communication.
A quick note about our weigh module kits specifically – we design them to work with all major PLCs: Allen-Bradley, Siemens, Omron, you name it. We even give free calibration templates for each, so you don’t have to fumble through the PLC’s menus. And if you run into trouble, our tech team picks up the phone at 8am to 8pm EST, no automated menus, no wait times.
Wait, let’s make sure I didn’t skip anything. Oh, safety! If you’re working with heavy loads, lock out/tag out the equipment before you start – don’t climb on a conveyor while it’s live just to tighten a wiring nut. That’s not a tip, that’s a rule.

Now, wrapping this up. Integrating a weigh module kit with a PLC isn’t rocket science, but it’s the small details that make it work. Skip the generic tutorials, follow the pre-work, use the right wiring, calibrate with a test weight, and filter that signal properly. If you’re in the market for a weigh module kit, or you’re stuck on an integration that’s been giving you trouble, hit us up. We don’t do pushy sales – we help you pick the right kit for your application, walk you through the integration step by step, and even do a remote check-in if you need it. No fluff, no fine print, just stuff that works for your operation.
Spindle Load Cells References:
- Load Cell Integration and Calibration Guidelines, Weigh Technology Association, 2022
- PLC Analog Signal Processing for Industrial Applications, International Society of Automation, 2021
- Industrial Wiring Best Practices for Weight Sensors, National Electrical Manufacturers Association, 2020
Ningbo Hechang Electric Co., Ltd.
As one of the most professional weigh module kits manufacturers and suppliers in China, we also support customized service. We warmly welcome you to buy advanced weigh module kits for sale here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No.66 Yongmao West Road, Ningbo, China
E-mail: info@hcesensor.com
WebSite: https://www.hechangsensor.com/
